


Get In Touch
Do you have a questions or an issues we can help you with?
Let’s talk about your project and how Dohre can help get your tools designed, manufactured and ready for the market.

Reading volume: 7364

Release time :2021-09-26
Estimated reading time:
End mills are available in different cutting geometries because flat surfaces, curved profiles, deep cavities, narrow slots, shoulders, and high-material-removal operations require different tool designs. Square, ball nose, corner radius, roughing, long-neck, micro-diameter, and special-profile end mills each produce a different machining result. This guide compares the most common types of end mills used in CNC machining, explains the features each cutter is designed to produce, and shows where each tool type is normally selected.
In CNC milling, the shape of the cutting end directly affects the surface and feature that a tool can produce. A cutter designed for flat-bottom slots will not create the same result as a tool designed for curved mold surfaces or reinforced shoulder machining.
Understanding the main types of end mills makes it easier to distinguish between square, ball nose, corner radius, roughing, long-neck, micro-diameter, thread, and special-profile cutters before selecting a tool for a specific CNC machining operation.
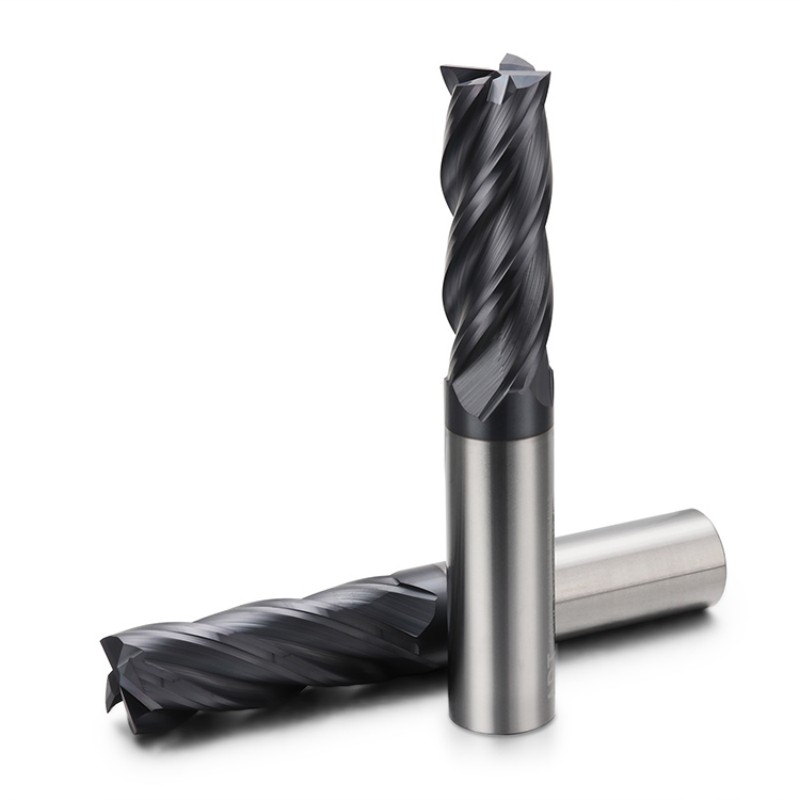
An end mill is a rotating cutting tool used in milling machines and CNC machining centers to remove material from a workpiece. Most end mills have cutting edges on the outside diameter and, depending on the tool design, across the end face.
This cutting structure allows an end mill to machine slots, pockets, side walls, shoulders, flat surfaces, curved profiles, and three-dimensional features. Different end geometries and flute designs are developed for different cutting results.
Dohre provides solid carbide end mills for CNC machining in multiple geometries, materials, coatings, flute configurations, and custom dimensions.
End mills can be classified by cutting-end geometry, flute design, tool reach, machining stage, and the type of feature they are designed to produce. The following are among the most common end mill types used in CNC metalworking.

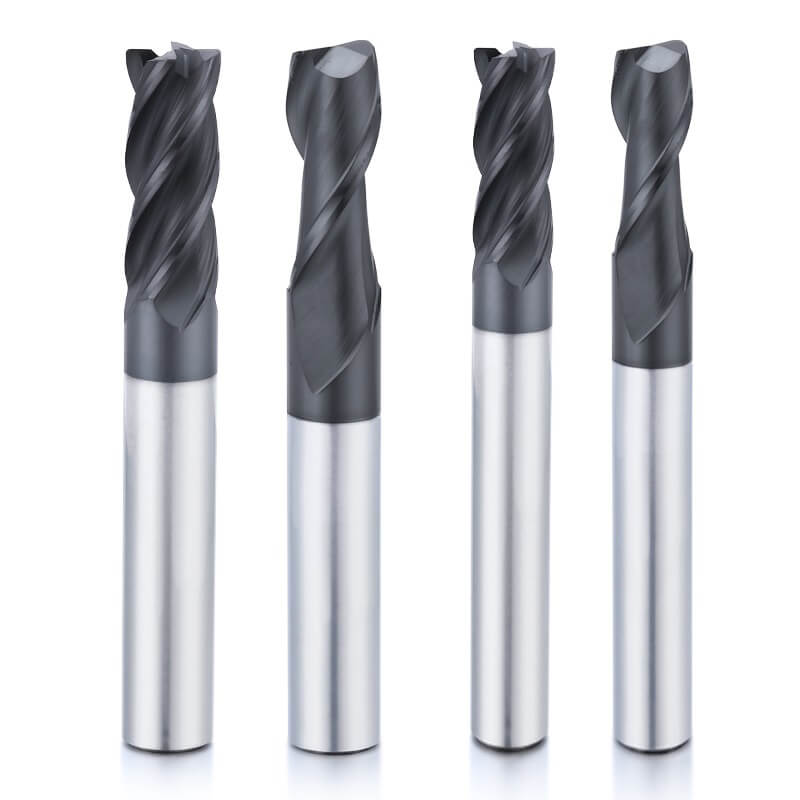
A square end mill, also called a flat end mill, has a flat cutting end with relatively sharp corners. It is commonly used for flat surfaces, full-width slots, pockets, straight side walls, shoulders, steps, and bottom-surface machining.
Square end mills are selected when the component requires a flat bottom or a clear bottom-to-wall transition. The sharp cutting corner provides accurate geometry, but it may be more sensitive to chipping during interrupted cutting, excessive engagement, or unstable machining.
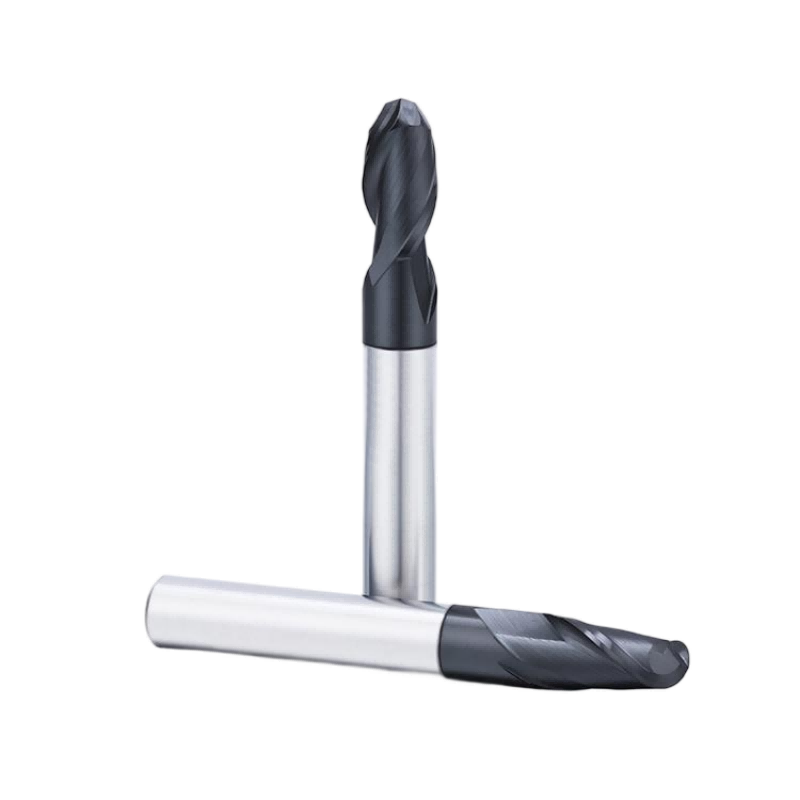
A ball nose end mill has a hemispherical cutting end. It is designed for curved surfaces, mold cavities, three-dimensional contours, freeform profiles, arc transitions, and detailed finishing operations.
The rounded cutting profile allows the tool to follow changing surface angles. Surface quality depends on the ball radius, step-over, toolpath, cutting engagement, runout, and cutting conditions near the tool center.
A corner radius end mill, sometimes called a bull nose end mill, has a mostly flat cutting end with a defined radius between the end face and the side cutting edge.
The corner radius reinforces the cutting edge and can reduce corner chipping compared with a sharp square end mill. These tools are commonly used for shoulders, side walls, steps, mold profiles, semi-finishing, and finishing operations requiring stronger corner support.
Roughing end mills use serrated or wave-shaped cutting edges to divide the removed material into smaller chip segments. This can reduce cutting pressure and support stable material removal during rough machining.
A roughing tool is normally used to remove the majority of the machining allowance before semi-finishing or finishing. It does not usually replace a dedicated finishing cutter when dimensional accuracy and final surface quality are important.
Finishing end mills are designed to support dimensional consistency, profile accuracy, and improved surface quality. They may use square, ball nose, or corner radius geometry depending on the required workpiece feature.
Finishing operations generally use smaller cutting engagement and require stable toolholding, suitable cutting parameters, controlled runout, and consistent cutting-edge quality.
A long-neck end mill has a reduced-neck section behind the cutting flutes. The reduced neck provides additional clearance for deep cavities, recessed surfaces, narrow openings, mold walls, and areas where the toolholder may interfere with the workpiece.
Long-neck tools are available with square, ball nose, and corner radius cutting ends. The neck should normally be only as long as required because unnecessary reach can increase vibration and tool deflection.
Micro-diameter end mills are designed for micro slots, small cavities, miniature shoulders, fine contours, optical-module features, electronic components, medical parts, precision mold inserts, and other small machining details.
Micro tools are particularly sensitive to spindle runout, toolholder accuracy, tool overhang, chip congestion, cutting depth, and entry method. Short and rigid tool configurations are generally preferred when the workpiece geometry permits.
A thread mill uses CNC helical interpolation to machine internal or external threads. Depending on the cutter design, one tool may produce different thread diameters when the pitch and tool geometry are suitable.
T-slot cutters are designed to produce T-shaped grooves after an access slot has been machined. Undercut cutters, lollipop cutters, dovetail cutters, and similar special tools reach features that cannot be machined with an ordinary straight end mill.
Other designs include straight-flute, tapered, V-shaped, double-ended, up-cut, down-cut, engraving, chamfering, and custom-profile cutters. Some of these geometries are used for plastics, composites, graphite, wood, engraving, trimming, and application-specific profile machining.
| End Mill Type | Typical Applications | Main Selection Reason |
|---|---|---|
| Square End Mill | Flat surfaces, slots, pockets, side walls and shoulders | Flat-bottom and sharp-corner geometry |
| Ball Nose End Mill | Curved surfaces, mold cavities and 3D contours | Continuous contact on curved profiles |
| Corner Radius End Mill | Shoulders, side walls, steps and profiles | Stronger cutting corner and edge protection |
| Roughing End Mill | High material removal and rough machining | Chip segmentation and reduced cutting pressure |
| Finishing End Mill | Final dimensional and surface finishing | Profile accuracy and surface consistency |
| Long-Neck End Mill | Deep cavities and restricted machining areas | Additional holder and workpiece clearance |
| Micro-Diameter End Mill | Micro slots, small cavities and miniature features | Access to small precision geometry |
| Thread Mill | Internal and external CNC thread machining | Flexible thread production by interpolation |
Square, ball nose, and corner radius end mills may have the same nominal cutting diameter, but they produce different workpiece features. The cutting-end profile determines how the tool contacts the bottom surface, side wall, corner transition, and curved profile.
| Geometry | Resulting Surface | Typical Application |
|---|---|---|
| Square End Mill | Flat bottom and straight side wall | Slots, pockets, shoulders and steps |
| Ball Nose End Mill | Curved surface and smooth 3D contour | Mold cavities, freeform profiles and contour finishing |
| Corner Radius End Mill | Flat area with a rounded corner transition | Shoulders, side walls, profiles and edge protection |
A square end mill is normally selected when a flat bottom and clear wall transition are required. A ball nose end mill is selected for continuously curved surfaces. A corner radius end mill provides a compromise between a flat cutting area and stronger corner support.
End mills are used to produce a wide range of surfaces and component features in steel, stainless steel, aluminum, titanium alloy, mold steel, hardened steel, graphite, plastics, composites, and other machinable materials.
| Machining Operation | Typical Use |
|---|---|
| Slotting | Producing full-width slots, grooves and channels |
| Side Milling | Machining vertical walls, edges and side surfaces |
| Pocketing | Removing material inside an enclosed boundary |
| Shoulder Milling | Producing a bottom surface and adjacent side wall |
| Profiling | Following an internal or external component contour |
| Surface Finishing | Improving surface quality and dimensional consistency |
| 3D Contouring | Machining molds, curved surfaces and freeform geometry |
| Deep Cavity Machining | Reaching recessed features with long-neck tools |
| Micro Machining | Producing miniature slots, cavities and precision details |
A more detailed explanation of individual operations is available in our guide to end mill machining operations and applications.
End milling is a machining process in which a rotating cutter removes material while the CNC machine moves the tool or workpiece along a programmed path. Cutting may occur on the outer diameter, end face, or both.
The cutting edges along the outer diameter perform peripheral cutting. These edges are primarily responsible for side milling, profiling, wall machining, and controlling slot or contour width.
The cutting edges on the end face machine bottom surfaces, slots, pockets, shoulders, and axial-entry features. The resulting bottom geometry depends on whether the cutter is square, ball nose, radius, or another profile.
A center-cutting end mill has cutting edges that reach or cross the tool center, allowing axial entry under suitable conditions. A non-center-cutting tool normally requires side entry, ramping, helical interpolation, or a pre-machined access hole.
Even when a cutter is center cutting, straight vertical plunging is not always the most suitable entry method. Tool geometry, diameter, material, cutting depth, chip evacuation, and machine rigidity must be considered.
The main parts of an end mill influence its cutting action, chip evacuation, rigidity, feature access, and dimensional capability.

| End Mill Part | Function |
|---|---|
| Cutting Diameter | Determines cutter size, slot width and minimum feature access |
| Flutes | Form the cutting edges and provide chip space |
| Peripheral Cutting Edge | Performs side milling, profiling and wall machining |
| End Cutting Edge | Machines bottom surfaces, slots and pockets |
| Core | Provides tool strength and supports the cutting edges |
| Helix Angle | Influences cutting force, edge engagement and chip flow |
| Flute Length | Determines the available axial cutting depth |
| Neck | Provides clearance for deep and restricted features |
| Shank | The cylindrical section held by the toolholder |
| Overall Length | The total length from the cutting end to the back of the shank |
Longer cutting sections and greater tool reach improve accessibility but may reduce rigidity. The shortest practical flute length, neck length, and tool overhang generally provide better machining stability.
End mills and drill bits are both rotating cutting tools, but they are designed for different cutting directions and machining operations.

| Feature | End Mill | Drill Bit |
|---|---|---|
| Main Purpose | Machining surfaces, slots, pockets and contours | Producing round holes |
| Cutting Direction | Axial and lateral, depending on geometry | Primarily axial |
| Cutting Edges | End-face and peripheral cutting edges | Drill point and cutting lips |
| Typical Operations | Slotting, profiling, pocketing and contouring | Drilling and hole making |
| Side Cutting | Designed for side cutting | Normally not designed for side milling |
A center-cutting end mill can enter the workpiece axially in suitable applications, but it is not automatically a replacement for a dedicated drill bit. Hole depth, chip evacuation, diameter accuracy, and bottom geometry must be considered.
Tool material affects cutting speed, rigidity, edge strength, wear resistance, heat resistance, and suitable machining applications.
High-speed steel end mills generally provide good toughness and a lower initial cost. They may be suitable for lower cutting speeds, less rigid machines, repair work, special tool shapes, and smaller production quantities.
Solid carbide end mills provide high hardness, rigidity, wear resistance, and cutting-edge stability. They are widely used in CNC machining where higher cutting speeds, dimensional consistency, surface quality, and stable batch production are required.
Carbide grade, cobalt content, coating, flute geometry, and edge preparation can be adjusted according to the workpiece material and machining conditions.
More information is available in our guide to the advantages of solid carbide end mills for high-speed CNC machining.
CBN and PCD tools are used for specialized applications rather than as direct replacements for ordinary carbide end mills. CBN is commonly considered for high-hardness steel finishing, while PCD can be used for selected non-ferrous, graphite, composite, and abrasive-material applications.
The required workpiece feature provides the first direction for selecting an end mill type. Material, flute count, coating, tool length, and machine conditions should then be evaluated separately.
| Machining Requirement | Recommended Tool Direction |
|---|---|
| Flat bottom or straight side wall | Square end mill |
| Curved or three-dimensional surface | Ball nose end mill |
| Shoulder with stronger cutting corner | Corner radius end mill |
| High stock removal | Roughing end mill |
| Deep or restricted feature | Long-neck end mill |
| Small precision feature | Micro-diameter end mill |
| Internal or external CNC thread | Thread mill |
End geometry is only the first stage of tool selection. Workpiece material, flute count, cutting length, coating, tool reach, machine rigidity, toolholder runout, and chip evacuation must also be considered.
Our complete end mill selection guide for CNC machining explains how to evaluate these factors together.
Flute count also affects chip space, core strength, and the number of cutting edges. See our comparison of 2 flute and 4 flute end mills for more detailed guidance.
Common types include square end mills, ball nose end mills, corner radius end mills, roughing end mills, finishing end mills, long-neck tools, micro-diameter end mills, thread mills, T-slot cutters, and special-profile cutters.
Square end mills are among the most widely used types because they can machine flat surfaces, slots, pockets, side walls, shoulders, and steps. The correct type still depends on the required workpiece feature.
A square end mill produces flat bottoms and relatively sharp transitions. A ball nose end mill follows curved and three-dimensional surfaces. A corner radius end mill provides a mostly flat cutting area with a reinforced rounded corner.
A square end mill is generally selected for flat-bottom surfaces, slots, shoulders, steps, and straight side walls.
A ball nose end mill is commonly used for curved surfaces, mold cavities, freeform profiles, arc transitions, and three-dimensional contour finishing.
A roughing end mill has serrated or wave-shaped cutting edges that divide the removed material into smaller chips. It is designed for stable material removal before semi-finishing or finishing.
A long-neck end mill is used when the cutting edge must reach a deep or restricted feature while avoiding interference between the toolholder and the workpiece.
End mills are used for slotting, pocketing, side milling, shoulder milling, profiling, surface finishing, three-dimensional contouring, deep cavity machining, and micro-feature machining.
A center-cutting end mill can enter the material axially under suitable conditions. However, a dedicated drill bit is normally more efficient for producing standard round holes, particularly when hole depth and chip evacuation are important.
Start with the feature that must be machined. Then consider the workpiece material, machining stage, flute count, tool diameter, cutting length, reach, coating, machine rigidity, chip evacuation, and required surface quality.
Different types of end mills are developed because flat surfaces, curved profiles, deep cavities, micro features, threads, undercuts, and roughing operations require different cutting geometries.
Square, ball nose, corner radius, roughing, long-neck, and micro-diameter end mills each solve a different machining problem. Choosing the correct cutter begins with understanding the surface and feature that the tool must produce.
Dohre manufactures standard and custom carbide end mills for industrial CNC machining. Cutting diameter, flute length, neck dimensions, shank size, overall length, flute number, carbide grade, coating, and cutting geometry can be developed according to customer requirements.
Send us your workpiece material, machining feature, tool diameter, cutting depth, required surface finish, machine conditions, and production quantity. Dohre can recommend a suitable standard end mill or develop a custom tool for your application.
Contact DohreDo you have a questions or an issues we can help you with?
Let’s talk about your project and how Dohre can help get your tools designed, manufactured and ready for the market.
By continuing to use the site you agree to our privacy policy Terms and Conditions.