Product Description

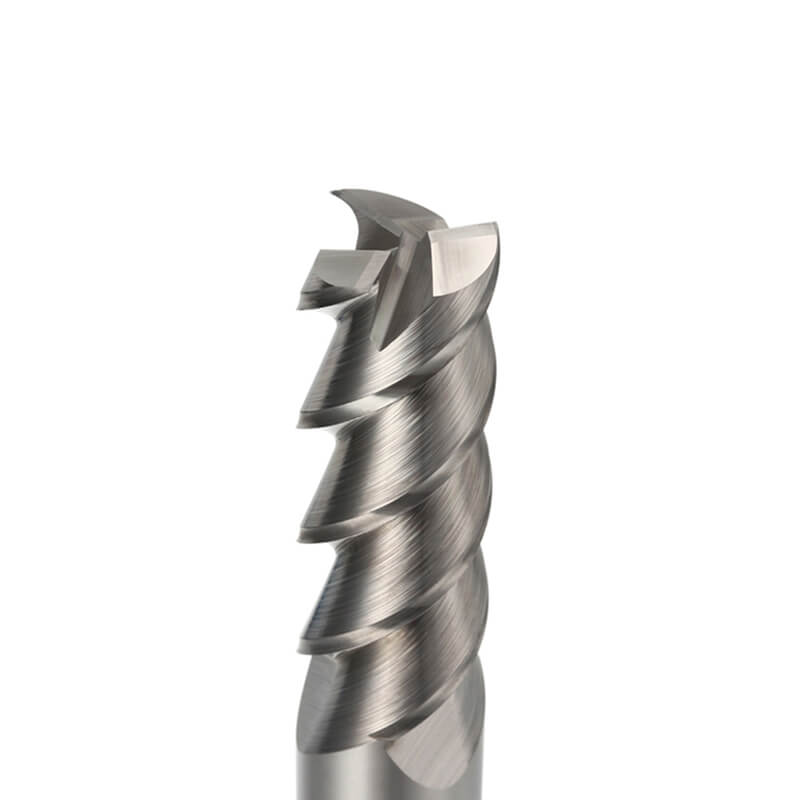
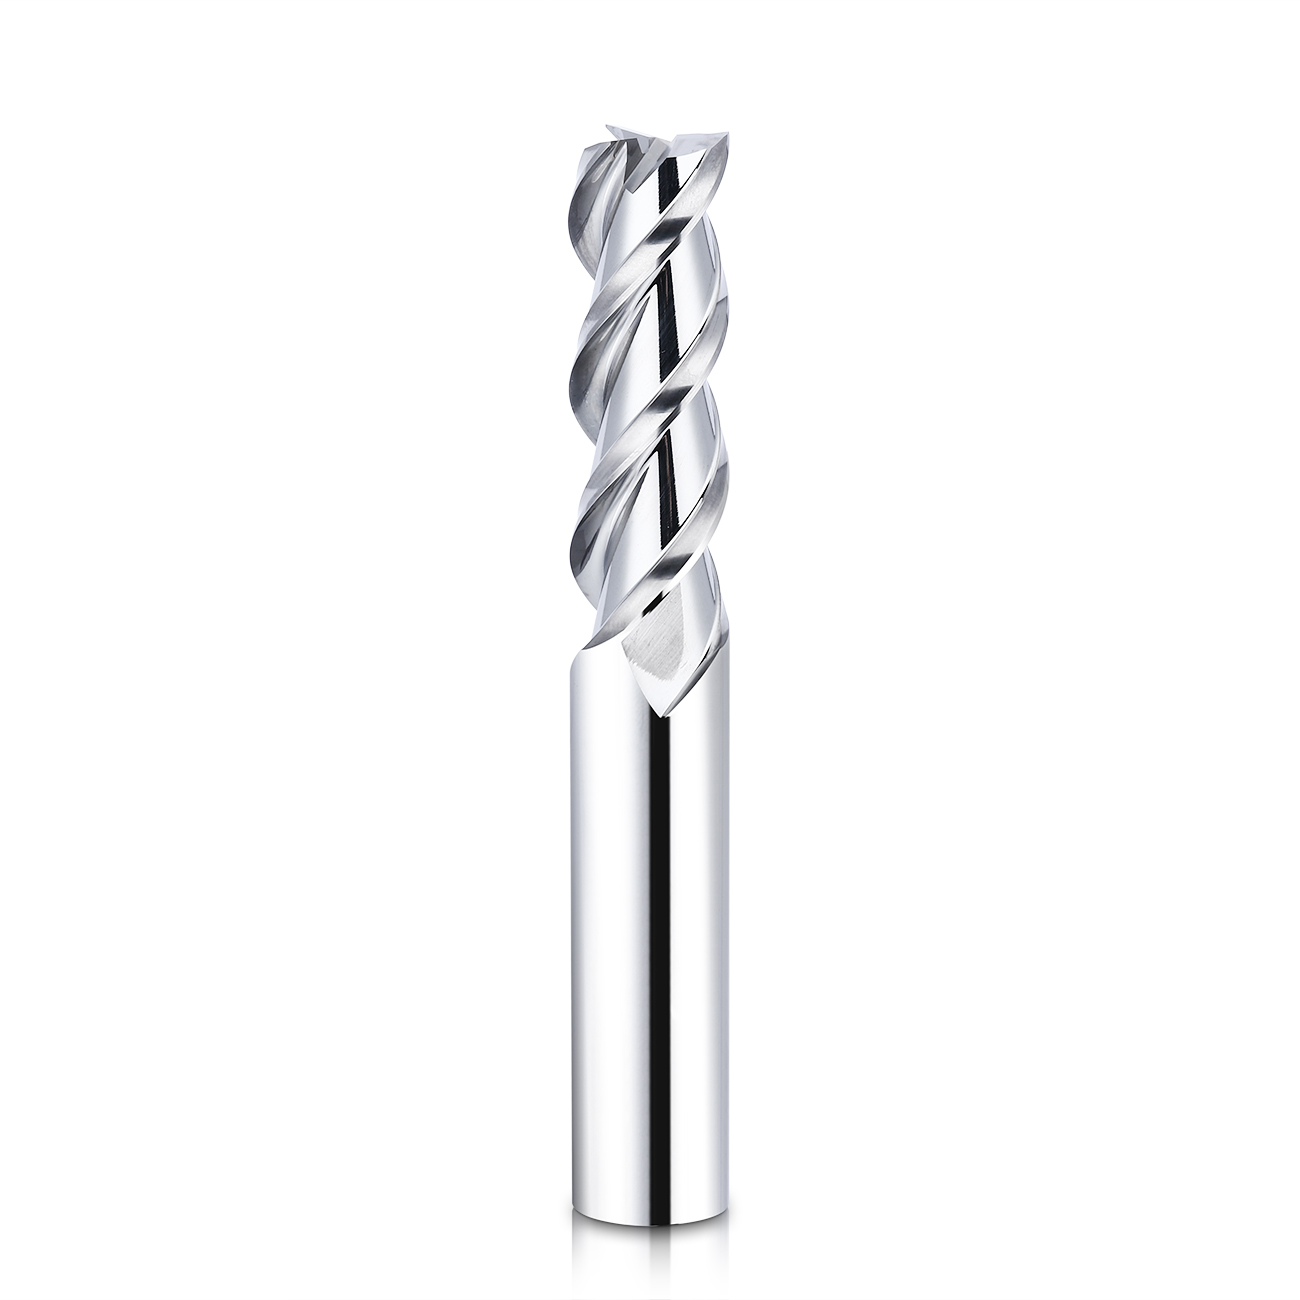
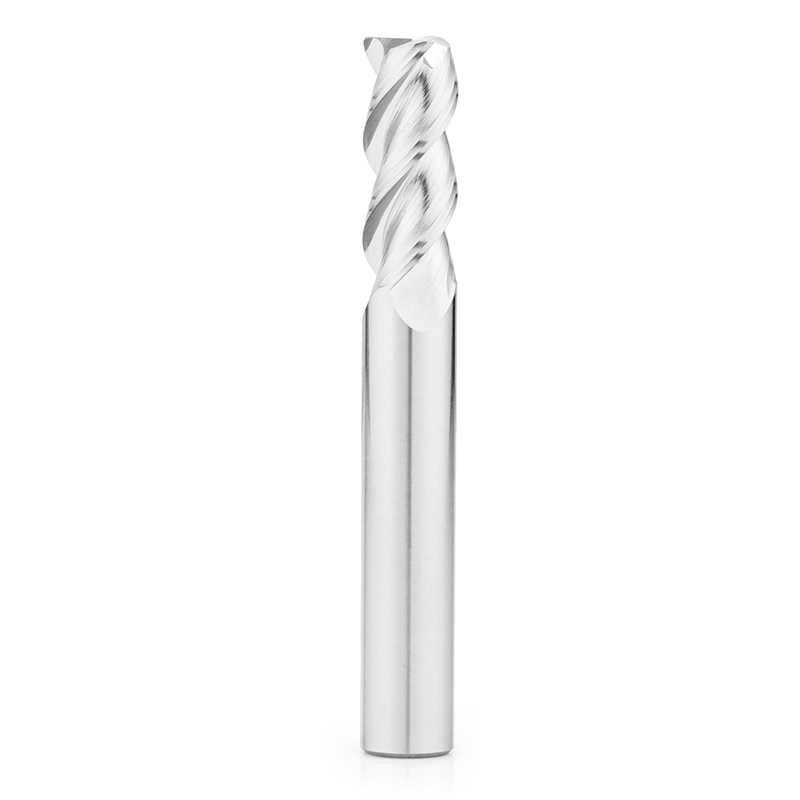
The DOHRE AEX square end mill is a solid carbide cutter designed for high-speed slotting, side milling, pocket machining, and shoulder milling of aluminum alloys such as 6061 and 7075. It is made from 0.8 μm fine-grain carbide with 10% cobalt and features a 45° helix angle, 55% core diameter, 6° end rake angle, and 12° side rake angle. Uncoated and DLC Rainbow coated versions are available.
Its positive rake geometry and 1200-grit precision-ground cutting edge are designed to support sharp cutting, smooth chip evacuation, and reduced cutting resistance. The square cutting profile is particularly suitable for slots, flat-bottom pockets, straight sidewalls, and defined shoulders.
For thin-wall aluminum components, the AEX square end mill can be used with controlled cutting engagement, short tool overhang, and stable workholding to help limit wall deflection and chatter. Actual performance depends on wall thickness, tool size, cutting parameters, and machine rigidity.
Product Features
Fine-Grain Carbide Material
The DOHRE AEX square end mill is manufactured from fine-grain carbide rods with a 0.8 μm grain size and 10% cobalt content. This carbide substrate provides a balance of hardness, toughness, and wear resistance for aluminum alloy and non-ferrous material machining.
Positive Rake Geometry
The AEX square end mill features a 6° end rake angle and a 12° side rake angle. This positive rake geometry is designed to support sharp cutting, lower cutting resistance, and reduced burr formation during aluminum slotting, side milling, and pocket machining.
Precision-Ground Cutting Edge
The cutting edge is precision-ground using a 1200-grit grinding wheel to support consistent edge sharpness and cutting geometry. A sharp cutting edge helps reduce cutting resistance and supports clean machining and surface quality when appropriate cutting conditions are maintained.
55% Core Diameter and 45° Helix Angle
The AEX square end mill features a 55% core diameter and a 45° helix angle. The smaller core design allows additional flute space for chip evacuation, while the high helix angle supports smoother cutting and chip flow during aluminum roughing, slotting, and high-speed milling.
Uncoated or DLC Rainbow Coating
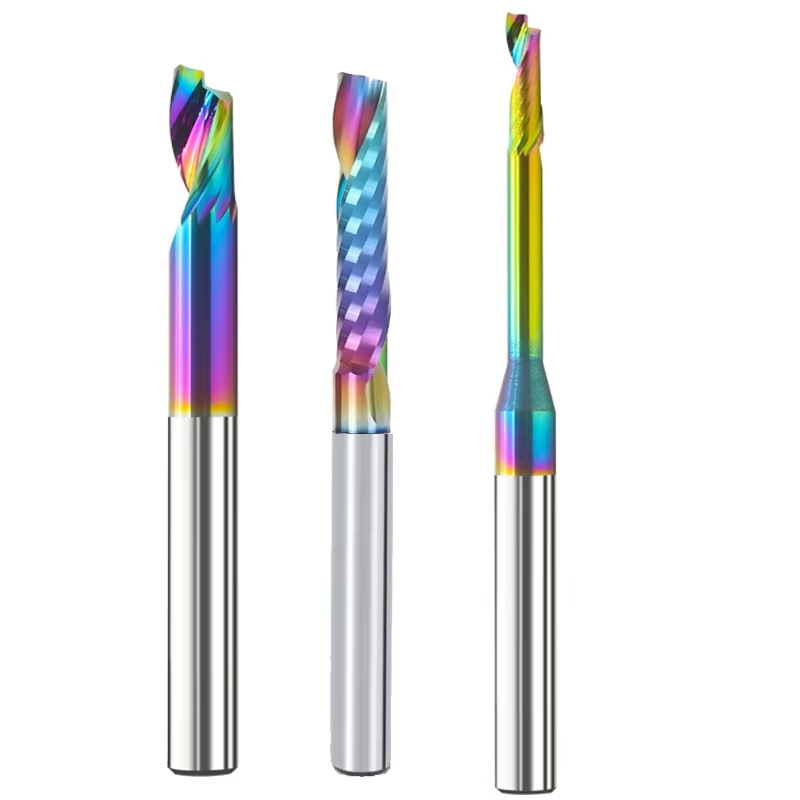
The DOHRE AEX square end mill is available in uncoated and DLC Rainbow coated versions. Both options are designed for aluminum machining, but the appropriate choice depends on material adhesion, cutting conditions, chip evacuation, and the required surface quality.
Uncoated vs DLC Rainbow: Which Is Better for Aluminum?
| Coating Option | Suitable Applications | Selection Considerations |
|---|
| Uncoated | General aluminum milling, slotting, and applications requiring a sharp cutting edge | Provides a sharp cutting edge without an additional coating layer. Effective chip evacuation and suitable lubrication help control aluminum adhesion and built-up edge. |
| DLC Rainbow | Aluminum milling applications where material adhesion, friction, or built-up edge is a concern | The low-friction DLC coating helps reduce aluminum adhesion and supports chip evacuation and surface quality under suitable cutting conditions. |
Selection Tip: Choose an uncoated end mill when a sharp cutting edge is the main priority and aluminum adhesion is adequately controlled. Consider DLC Rainbow coating when material sticking, built-up edge, or friction affects machining performance. Neither option is universally better for every aluminum alloy or operation.
Aluminum adhesion is a common challenge during high-speed milling and deep slotting. Learn more in our guide: Why Does Aluminum Stick to an End Mill?
Slotting, Side Milling and Pocket Machining Applications
AEX square end mills are especially suitable for aluminum machining tasks where chip evacuation, edge sharpness, and cutting efficiency are important.
| Machining Need | Why Use AEX Square End Mill |
|---|
| Slotting | Square end geometry helps machine straight slots and flat bottoms |
| Side milling | Sharp cutting edge supports clean side walls and stable cutting |
| Pocket machining | Large chip space improves chip evacuation in pocket features |
| Shoulder machining | Square end design helps maintain clear shoulder edges |
| Flat surface milling | Suitable for flat bottom surfaces and general aluminum milling |
| Roughing and semi-finishing | 55% core and 45° helix support smoother chip removal |
Suitable materials include:
•6000 series aluminum alloys
•6061 aluminum
•7000 series aluminum alloys
•7075 aluminum
•Aluminum-silicon alloys
•Magnesium alloys
•Copper alloys
•Engineering plastics
For 6061 aluminum machining, sharp cutting edges and smooth chip evacuation are important for reducing burrs and improving surface finish. More selection details can be found in: Best End Mill for 6061 Aluminum
For harder aluminum alloys such as 7075, coating selection, tool rigidity, and cutting parameters become more important. Related guide: Best End Mill for 7075 Aluminum
For users comparing flute designs in aluminum milling, this guide may also help: 2 Flute vs 3 Flute End Mill for Aluminum
Typical applications include:
•Aluminum slotting
•Side milling
•Pocket machining
•Shoulder machining
•Flat surface milling
•Aluminum roughing
•Semi-finishing of aluminum parts
•High-speed CNC milling of aluminum components
•Aerospace, automotive, electronics, mold, and precision machining applications
Thin-Wall Aluminum Milling and Chatter Control
Thin-wall aluminum components, especially those made from 6061 and 7075 alloys, can deflect or vibrate when cutting forces are too high. This may lead to chatter marks, dimensional errors, burr formation, and inconsistent surface finish.
The AEX square end mill uses positive rake geometry, a 45° helix angle, and a 55% core diameter to support lower cutting resistance and efficient chip evacuation. These features make it a suitable option for thin-wall side milling when tool engagement and workholding are properly controlled.
Recommended machining practices:
• Leave a consistent finishing allowance after roughing.
• Use controlled radial engagement to limit cutting forces and wall deflection.
• Minimize tool overhang and use rigid, accurate toolholding.
• Support thin sections with suitable fixtures or workholding methods.
• Maintain effective chip evacuation to prevent chip recutting.
• Adjust spindle speed, feed, and cutting depth according to wall thickness, tool diameter, and machine stability.
For thin aluminum walls, a sharp cutting edge alone cannot eliminate chatter. Toolpath strategy, cutting engagement, workholding, and machine rigidity must also be considered.
Manufacturing & Quality Control
DOHRE focuses on precision grinding, edge consistency, dimensional stability, and strict inspection for aluminum machining tools. AEX series end mills are produced under controlled manufacturing processes to support stable cutting performance and reliable batch quality.
German Walter 5-Axis Grinding Machines
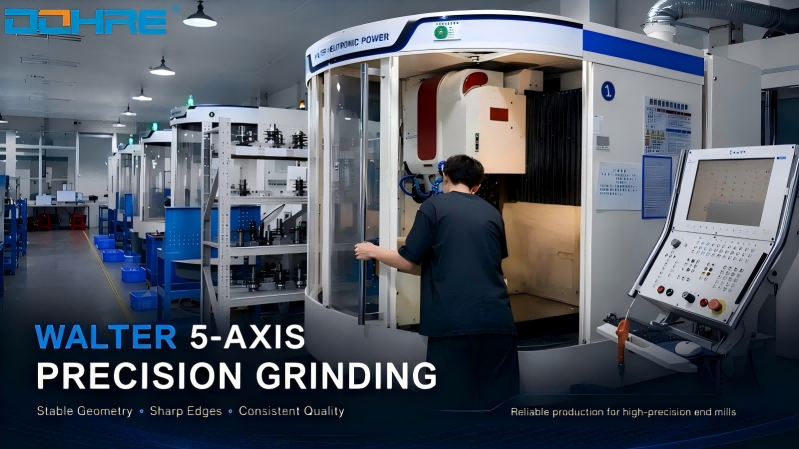
AEX series end mills are produced using German Walter 5-axis high-precision grinding machines. This helps maintain accurate flute geometry, stable dimensions, and consistent cutting edge quality.
Walter HELICHECK PLUS Inspection
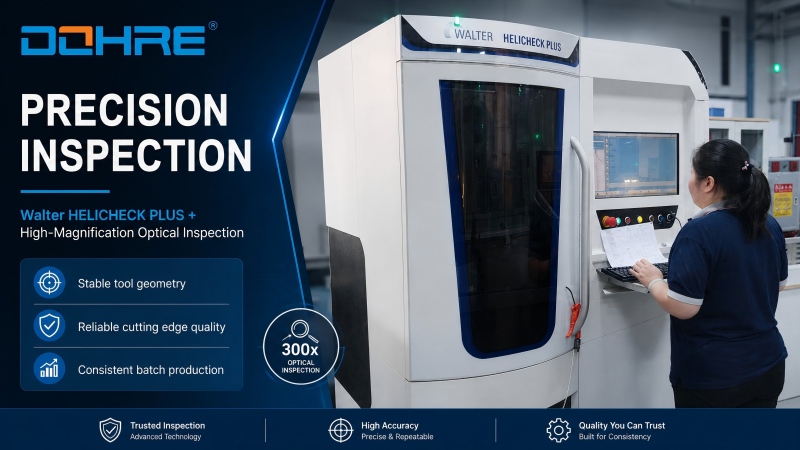
Tool profile accuracy is inspected using German Walter HELICHECK PLUS measuring equipment. Profile accuracy can be controlled within 5 μm, helping ensure stable tool geometry and consistent machining accuracy.
50× Microscope Inspection
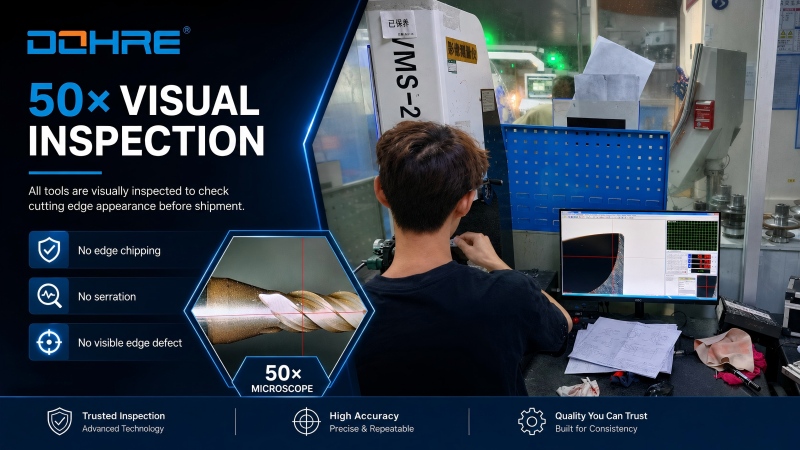
All tools are visually inspected under a 50× microscope to check cutting edge appearance. This helps ensure there is no edge chipping, serration, or visible cutting edge defect before shipment.
Stable Batch Quality
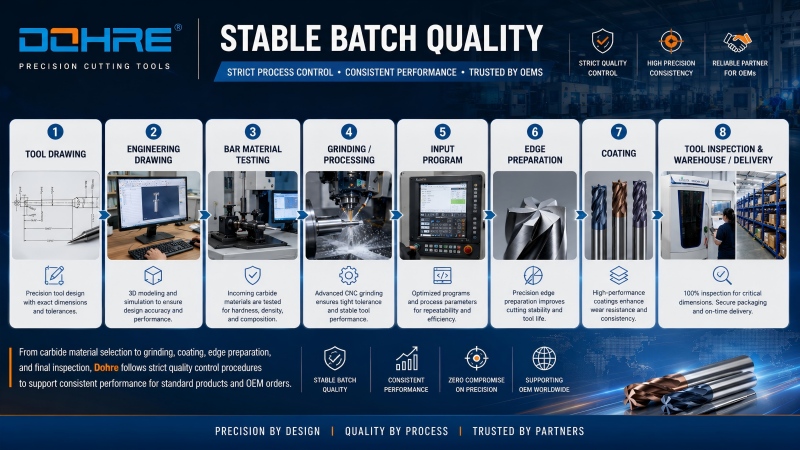
From carbide material selection to grinding, coating, edge inspection, and final quality control, DOHRE follows strict production procedures to support consistent performance for standard products and OEM orders.
FAQ & Contact us
Q1: What is the AEX square end mill used for?
The DOHRE AEX square end mill is designed for aluminum machining, particularly high-speed slotting, side milling, pocket machining, shoulder milling, and flat surface milling. Its sharp cutting geometry and optimized flute design support chip evacuation and stable cutting in aluminum alloys such as 6061 and 7075.
Q2: Can this square end mill machine 6061 aluminum?
Yes. The AEX square end mill is suitable for 6000-series aluminum alloys, including 6061. Its positive rake geometry and precision-ground cutting edge are designed to support sharp cutting and smooth chip evacuation. Appropriate cutting parameters and effective chip removal help control burr formation and maintain surface quality.
Q3: Can it be used for 7075 aluminum?
Yes. The AEX square end mill can be used for 7000-series aluminum alloys, including 7075. Suitable toolholding, coating selection, cutting engagement, and chip evacuation are important for maintaining cutting stability and tool life. Actual cutting parameters should be adjusted according to the material condition, tool diameter, and machining operation.
Q4: Should I choose an uncoated or DLC Rainbow coated end mill for aluminum?
For general aluminum machining, an uncoated AEX end mill provides a sharp cutting edge and can be suitable when chip evacuation and material adhesion are well controlled. The DLC Rainbow coated version is an option when aluminum sticking, friction, or built-up edge is a concern. Coating selection should consider the aluminum grade, cutting conditions, lubrication, and required surface quality.
Q5: Is the AEX square end mill suitable for slotting aluminum?
Yes. The AEX square end mill features a 55% core diameter and a 45° helix angle, designed to balance tool strength and flute space for chip evacuation. It is suitable for aluminum slotting and pocket machining when the cutting depth, feed rate, and chip removal method are properly selected. Full-width slotting requires particular attention to chip evacuation and cutting load.
Q6: What is the difference between a square end mill and a ball nose end mill for aluminum?
A square end mill is generally preferred for flat surfaces, flat-bottom pockets, slots, straight sidewalls, and defined shoulders. A ball nose end mill is better suited for curved surfaces, 3D contours, complex profiles, and surface finishing. The appropriate cutter depends on the workpiece geometry and machining stage.
Q7: Can DOHRE provide customized AEX square end mills?
Yes. DOHRE supports OEM and custom carbide end mill manufacturing, including cutting diameter, flute length, overall length, shank dimensions, coating options, and special cutting geometries. Customers can provide technical drawings, aluminum material grades, or machining requirements for evaluation. Our standard MOQ is 10 pieces, while available stock products may be ordered from 1 piece, subject to inventory confirmation.
Q8: How do I avoid chatter when milling thin aluminum walls?
To reduce chatter when milling thin aluminum walls, use controlled radial engagement, a consistent finishing allowance, short tool overhang, and stable workholding. The AEX square end mill features positive rake geometry, a 45° helix angle, and a 55% core diameter to support efficient cutting and chip evacuation. However, tool geometry alone cannot eliminate chatter. Wall thickness, toolpath strategy, spindle speed, cutting forces, and machine rigidity must also be considered.
Q9: Can I dry-mill aluminum with AEX end mills?
Dry milling may be possible in certain aluminum applications, depending on the alloy, cutting engagement, tool geometry, and chip evacuation conditions. Aluminum chips can adhere to the cutting edge or accumulate in slots and pockets, so reliable chip removal is important. Air blast, minimum quantity lubrication (MQL), or suitable coolant may be considered according to the operation and machine setup. Dry cutting should be evaluated for the specific application rather than assumed suitable for every aluminum milling process.
Q10: Is a single-flute, 2-flute, or 3-flute end mill better for aluminum?
The best flute count depends on the aluminum alloy, machining operation, cutting speed, and chip evacuation requirements. Single-flute end mills offer generous chip space and can be suitable for high-speed cutting in selected applications. Two-flute end mills provide substantial chip clearance for slotting and general aluminum milling. Three-flute end mills can offer a balance between chip evacuation and cutting-edge engagement for suitable high-speed operations. Availability of each flute configuration should be confirmed for the selected AEX tool model.